Stainless Steel Fabrication & Laser Processing in Singapore
Drawing-based stainless steel parts for prototypes, replacement components and repeat production. We review the grade, thickness, geometry, finish and inspection requirements before confirming the manufacturing route.
Choose the grade around the environment and the full fabrication route
304 is widely used for general industrial, indoor and sheltered equipment parts. 316 is commonly considered when chloride, salt, chemical or frequent wash-down exposure raises the corrosion risk. The low-carbon 304L and 316L variants may be preferred where welding and the project specification make sensitisation control important.
201 can suit selected cost-sensitive applications, but it should not be treated as an automatic substitute for 304 or 316. Grade selection must also consider surface condition, fabrication contamination, crevices, drainage, cleaning and maintenance.
Read the detailed 304 vs 316 guide →Stainless steel grades we review
The table is a starting point, not a substitution rule. Use the grade, condition and applicable material standard stated by the responsible engineer or drawing.
| Grade | General positioning | Fabrication considerations | Do not assume |
|---|---|---|---|
| 201 | Selected cost-sensitive indoor and general-use components. | Confirm forming, finish and the real service environment before substitution. | That it can directly replace 304 in chloride or corrosive exposure. |
| 304 | Common equipment panels, covers, brackets, trays and general industrial parts. | Widely fabricated; surface finish and cosmetic-face protection still need specification. | That one grade is automatically suitable for every outdoor location. |
| 304L | 304-family applications where welding or the material specification calls for a low-carbon grade. | Weld design, heat input and post-weld surface treatment remain important. | That “L” simply means a universally stronger version of 304. |
| 316 | Projects with higher chloride, salt, chemical or wash-down exposure risk. | Molybdenum improves pitting resistance, but crevices and contamination still matter. | That 316 is immune to corrosion or needs no cleaning and maintenance. |
| 316L | 316-family welded fabrications and specifications requiring low carbon. | Confirm welding, surface restoration, certification and inspection scope. | That the material grade alone proves medical, cleanroom or marine compliance. |
From flat profiles to multi-face tube features
The suitable process depends on the stock form as well as the finished geometry. Send the actual profile, thickness or wall thickness rather than a generic “stainless steel” description.
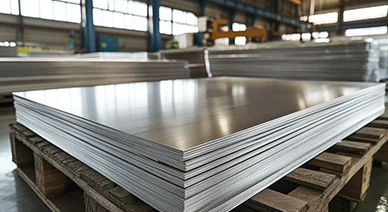
Sheet & plate
Flat profiles, holes, slots, tabs and cut-outs for panels, brackets, covers and blanks that may proceed to forming or assembly.
Sheet metal laser cutting →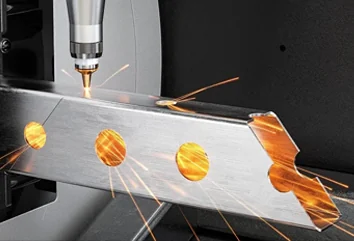
Tube & profile
Round, square and rectangular profiles with end cuts, holes, slots, notches and features distributed across more than one face.
Tube and profile cutting →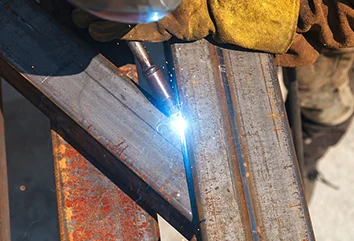
Fabricated assemblies
Cut parts can be coordinated with bending, welding, deburring, marking and finishing when the drawing defines the assembly and acceptance requirements.
Welding and assembly →Capabilities for stainless steel parts
A finished component often needs more than one operation. The drawing should communicate how cutting, forming, joining, marking and finishing affect the final fit and surface.
Laser cutting
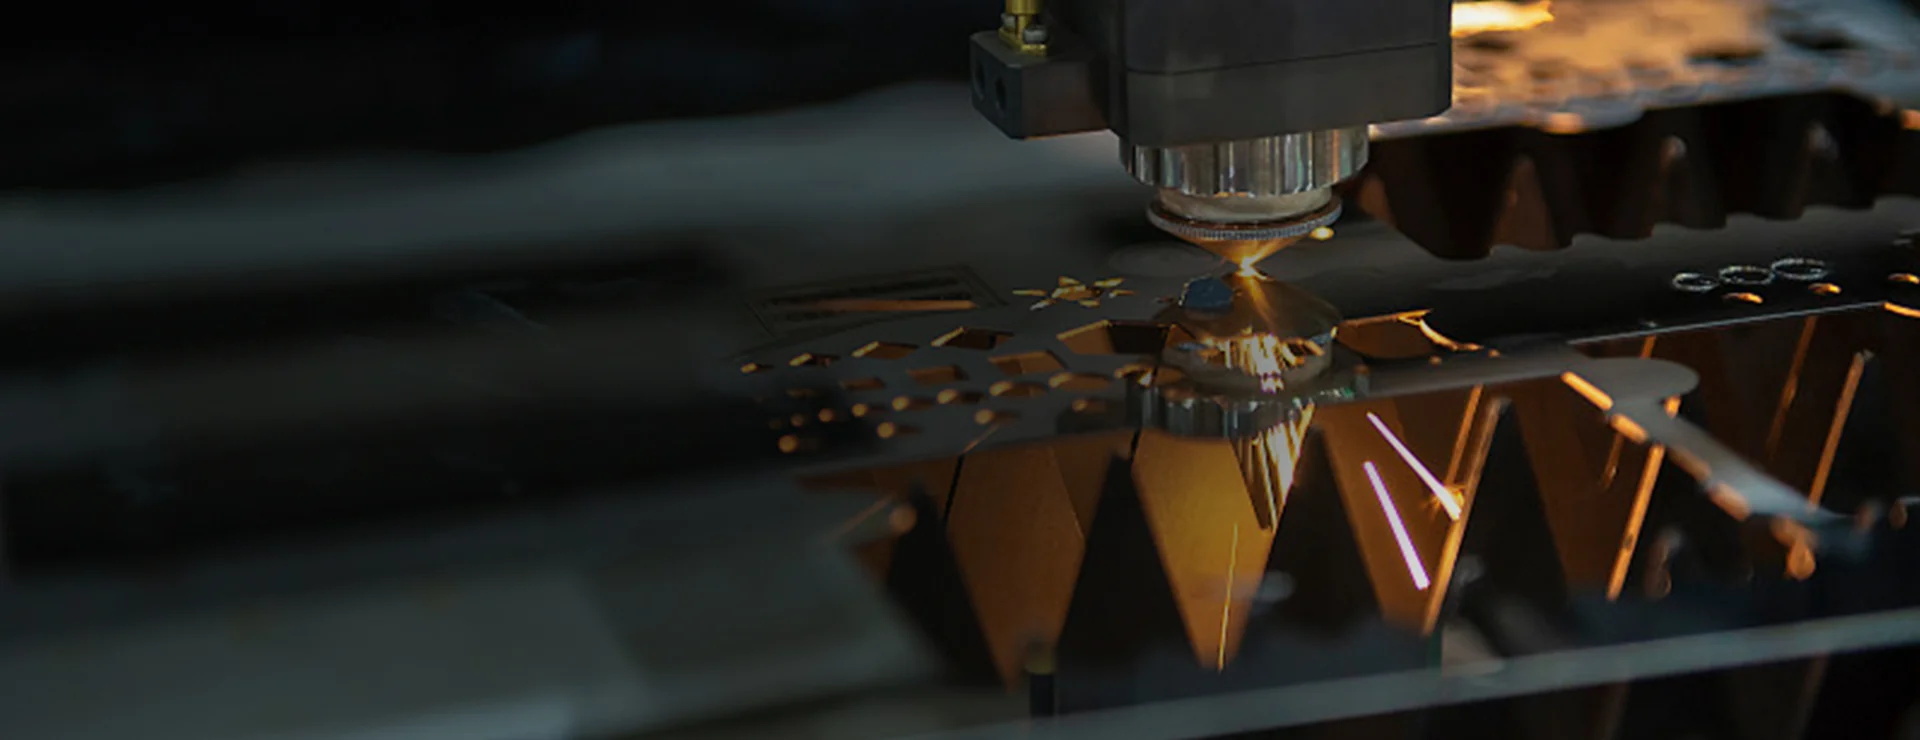
Profiles, holes, slots and cut-outs for flat or tubular parts. Grade, thickness, surface condition, feature size, gas strategy and downstream use all influence the edge.
Thickness and edge guide →
CNC bending
Formed brackets, channels, covers and enclosures require a suitable inside radius, bend allowance, relief geometry and control of cosmetic surfaces.
CNC bending capability →
Welding & assembly
Joint design, heat input, restraint, distortion, heat tint and required post-weld treatment should be planned together rather than checked only after welding.
Welding and assembly →
Laser marking & engraving
Part numbers, logos, serial data and machine-readable codes need an agreed mark type, position, contrast, depth and verification method.
Laser marking capability →
Polishing & grinding
Deburring, weld blending, brushed appearance and local finishing should define the cosmetic face, grain direction and acceptable variation.
Polishing and grinding →
Inspection to drawing
Inspection scope can cover dimensions, datums, feature position, flatness, surface condition, assembly and marking when these requirements are defined before production.
Quality assurance →Nitrogen or oxygen for stainless steel?
Nitrogen is commonly considered where a cleaner-looking, lower-oxidation cut edge is important. Oxygen changes the chemistry and appearance of the cut edge and may add preparation before selected downstream processes.
Gas choice still depends on thickness, equipment, productivity, edge requirements and the operations that follow. Nitrogen cutting is not passivation and does not automatically certify corrosion performance or cleanliness.
Compare Assist GasesOften selected for low-oxidation stainless edges, visible components and routes that proceed to welding, polishing or finishing.
A reactive cutting route whose edge condition and downstream preparation must be evaluated for the actual part and application.
Stainless steel components across industrial projects
These examples describe common part types, not automatic compliance claims. Regulatory, hygienic, structural or industry-specific requirements must be stated in the project specification.
 Automation frames & supports
 Equipment housings & covers
 Railings & infrastructure parts
 Nameplates & traceability partsBent brackets & channelsWelded assembliesTube profiles with holes & notchesPanels, plates & flat profiles
Plan for exposure—not just the word “stainless”
Singapore’s humidity, coastal salt, sheltered crevices, wash-down chemicals and outdoor drainage can change the corrosion risk. 316 may be considered where chloride exposure is significant, but grade selection alone does not prevent corrosion.
For safety-critical, structural, pressure, hygienic or regulated applications, the responsible engineer should confirm the material specification and acceptance criteria.
Define inspection before production
A machine’s positioning specification is not the same as guaranteed part accuracy. Inspection should follow the functional drawing, agreed datums and the actual manufacturing stage.
State critical characteristics, tolerances, datums and required documentation in the RFQ. Items not defined on the drawing may be interpreted differently by design, production and inspection teams.
What to send for a stainless steel quotation
Clear inputs reduce assumptions and help the team review material, cutting, forming, finishing and inspection as one route.
Related stainless steel services and guides
Stainless steel fabrication questions
Should I choose 304 or 316 stainless steel?
304 is widely used for general industrial, indoor and sheltered parts. 316 is commonly considered where chloride, salt, chemical or repeated wash-down exposure increases corrosion risk. Final selection should account for the complete environment, design, finish and customer specification—not grade name alone.
What is the difference between 304 and 304L?
304L is a low-carbon variant within the 304 family and may be specified for welded fabrication to reduce sensitisation-related concerns. It is not simply a universally stronger version of 304. Follow the drawing, applicable material standard and engineering requirement.
Can sheet and tube parts be supplied in the same project?
They can be reviewed as one coordinated fabrication project when the RFQ identifies each material form, grade, thickness or wall thickness, quantity, assembly relationship and inspection requirement.
Does nitrogen cutting remove every oxidation or finishing concern?
No. Nitrogen is commonly selected to limit cut-edge oxidation, but the final edge still depends on equipment setup, thickness, gas quality, material condition and feature geometry. Nitrogen cutting is not passivation, polishing or a cleanliness certification.
Can laser-cut holes be used directly for precision fits?
Some clearance holes may be used as cut, but locating-pin, bearing, threaded and close-fit holes require individual review. Hole diameter, thickness, taper, roundness and the functional tolerance may make drilling, reaming, tapping or CNC finishing necessary.
What files should I send for a quotation?
Send a DXF for flat profiles, a STEP model for formed or multi-face parts, and a PDF drawing showing grade, thickness, quantities, tolerances, datums, finish, welding, marking and inspection notes. Identify which file governs if the files conflict.
Turn the material specification into a manufacturable part
Share the drawing, stainless grade, thickness, quantity and required finish for a project-specific review.